How to Choose Your First 3D Printer: Buying Guide 2026
Published October 31, 2026
Products in this guide
In this article
Choose a first 3D printer by project size, repeatable first layers, compatible filament and repair parts. Giant speed figures and bundles cannot fix poor adhesion, unsafe placement or limited material support. Start with a manageable FDM machine for organizers and prototypes; bigger or heat-resistant jobs require more space and sometimes an enclosure [1][2][3].
Is a 3D printer worth it in 2026?
Worth it for repeat projects and learning CAD. FDM printing can create cable clips, organizers, hobby models, prototypes and non-safety-critical replacement parts.
Skip it if you need a single part, lack a suitable ventilated area, or need a load-bearing safety component. A service avoids setup and maintenance. Do not assume a PLA or PETG print is food-safe, flame-retardant or load-rated merely because a filament seller advertises the base material.
What actually matters
1. Build volume and the space the machine actually occupies
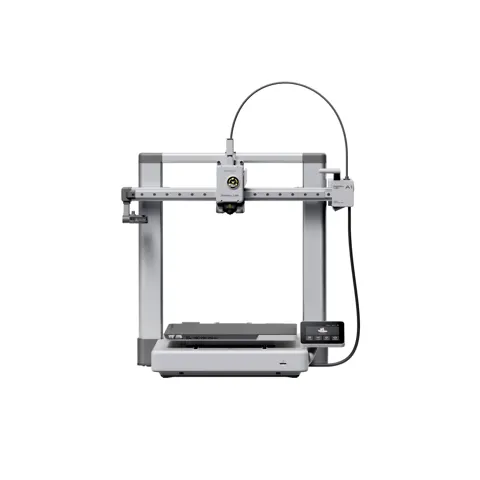
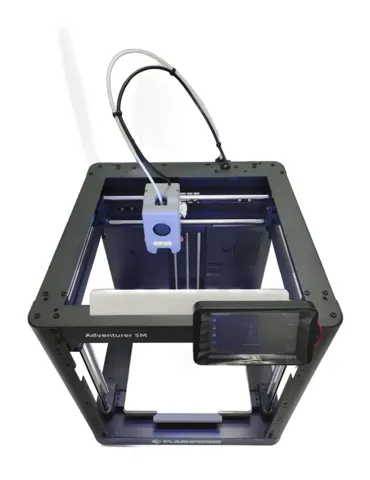
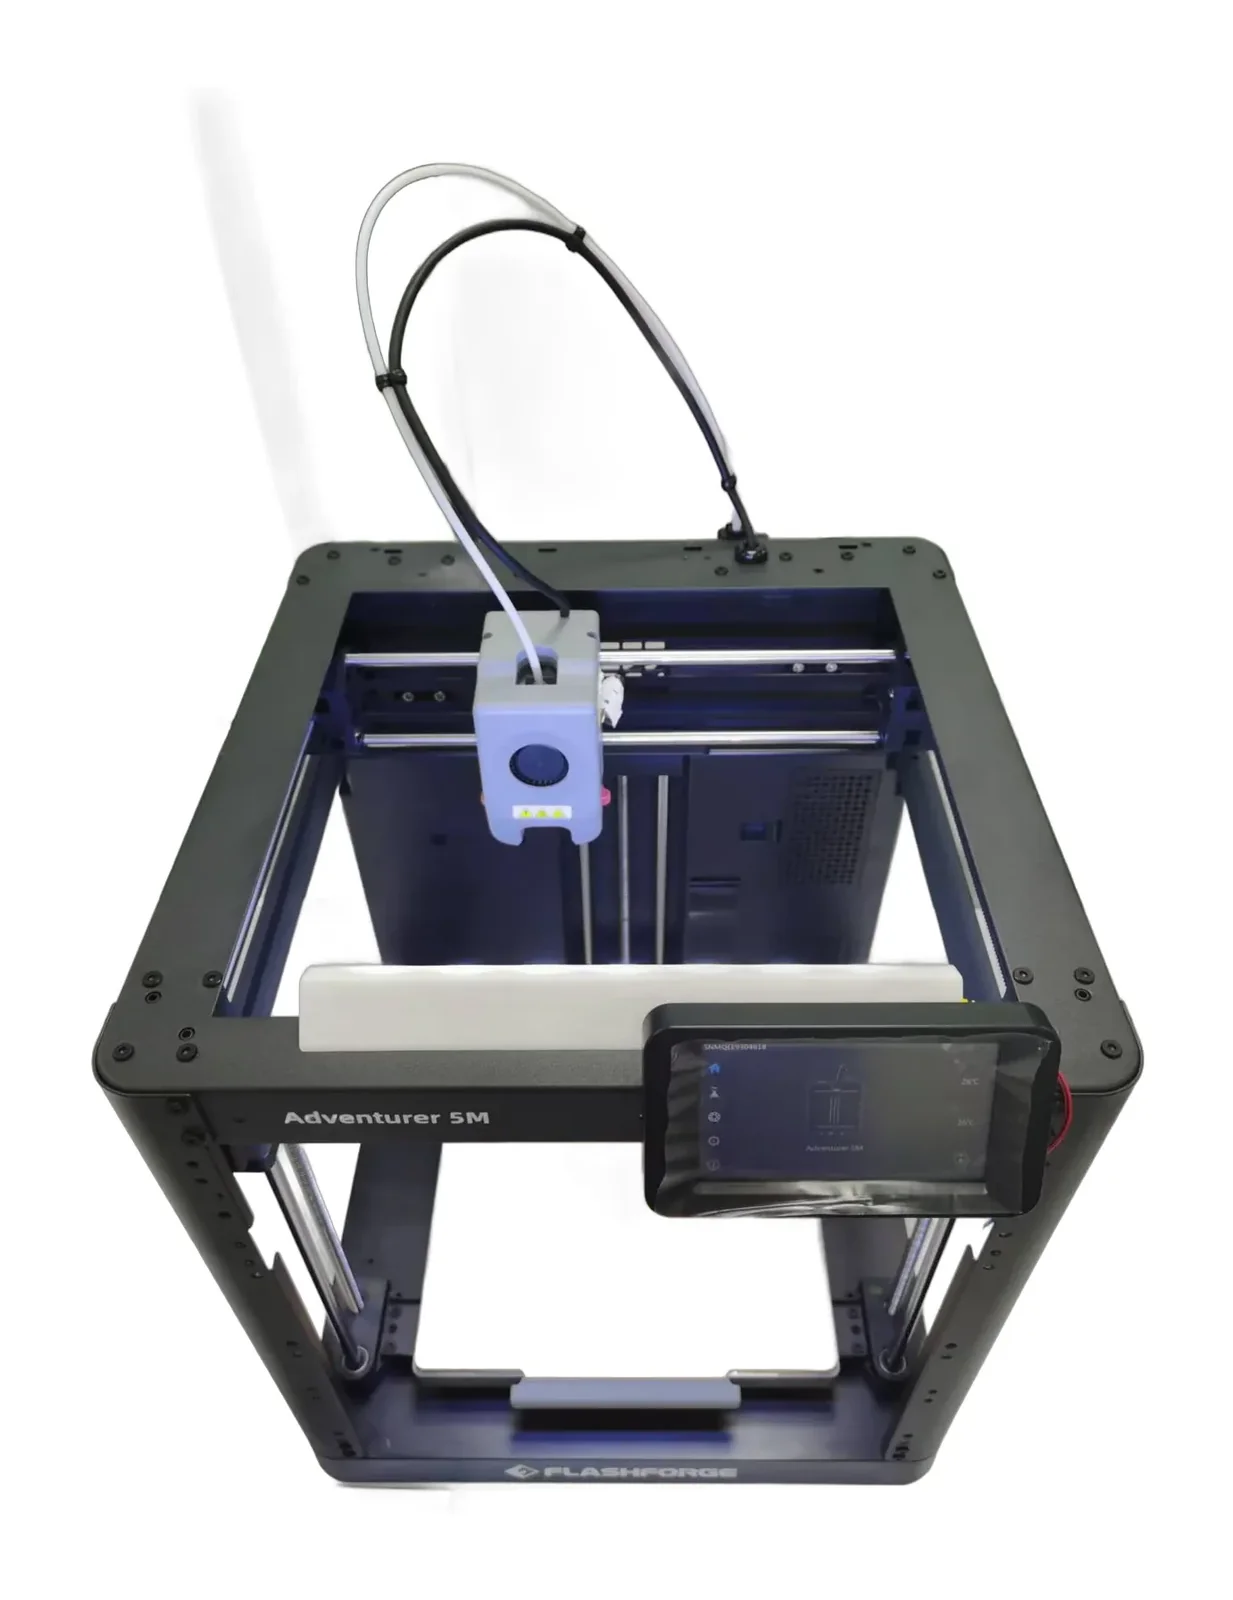
Build volume means X × Y × Z in millimeters, not the printer’s outer dimensions. The Bambu Lab A1 mini offers 180 × 180 × 180 mm [1]; the FlashForge Adventurer 5M has 220 × 220 × 220 mm [3]; the Bambu Lab A1 extends to 256 × 256 × 256 mm [4]. Choose against real model dimensions, not a hypothetical future giant project.
A 205 mm part cannot fit along a 180 mm axis without rotation, splitting or redesign. Brims and supports also consume room. For occasional large objects, dividing a model and assembling it can be more practical than dedicating permanent space to a larger printer.
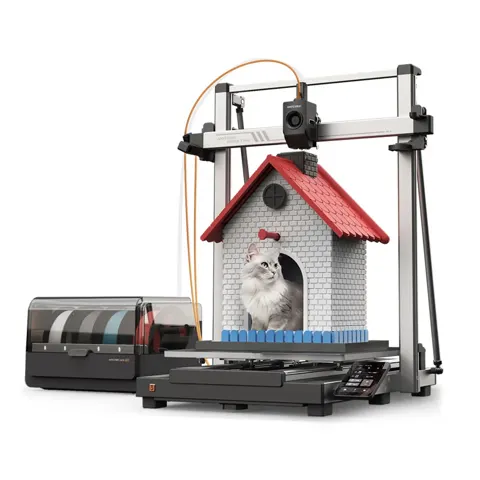
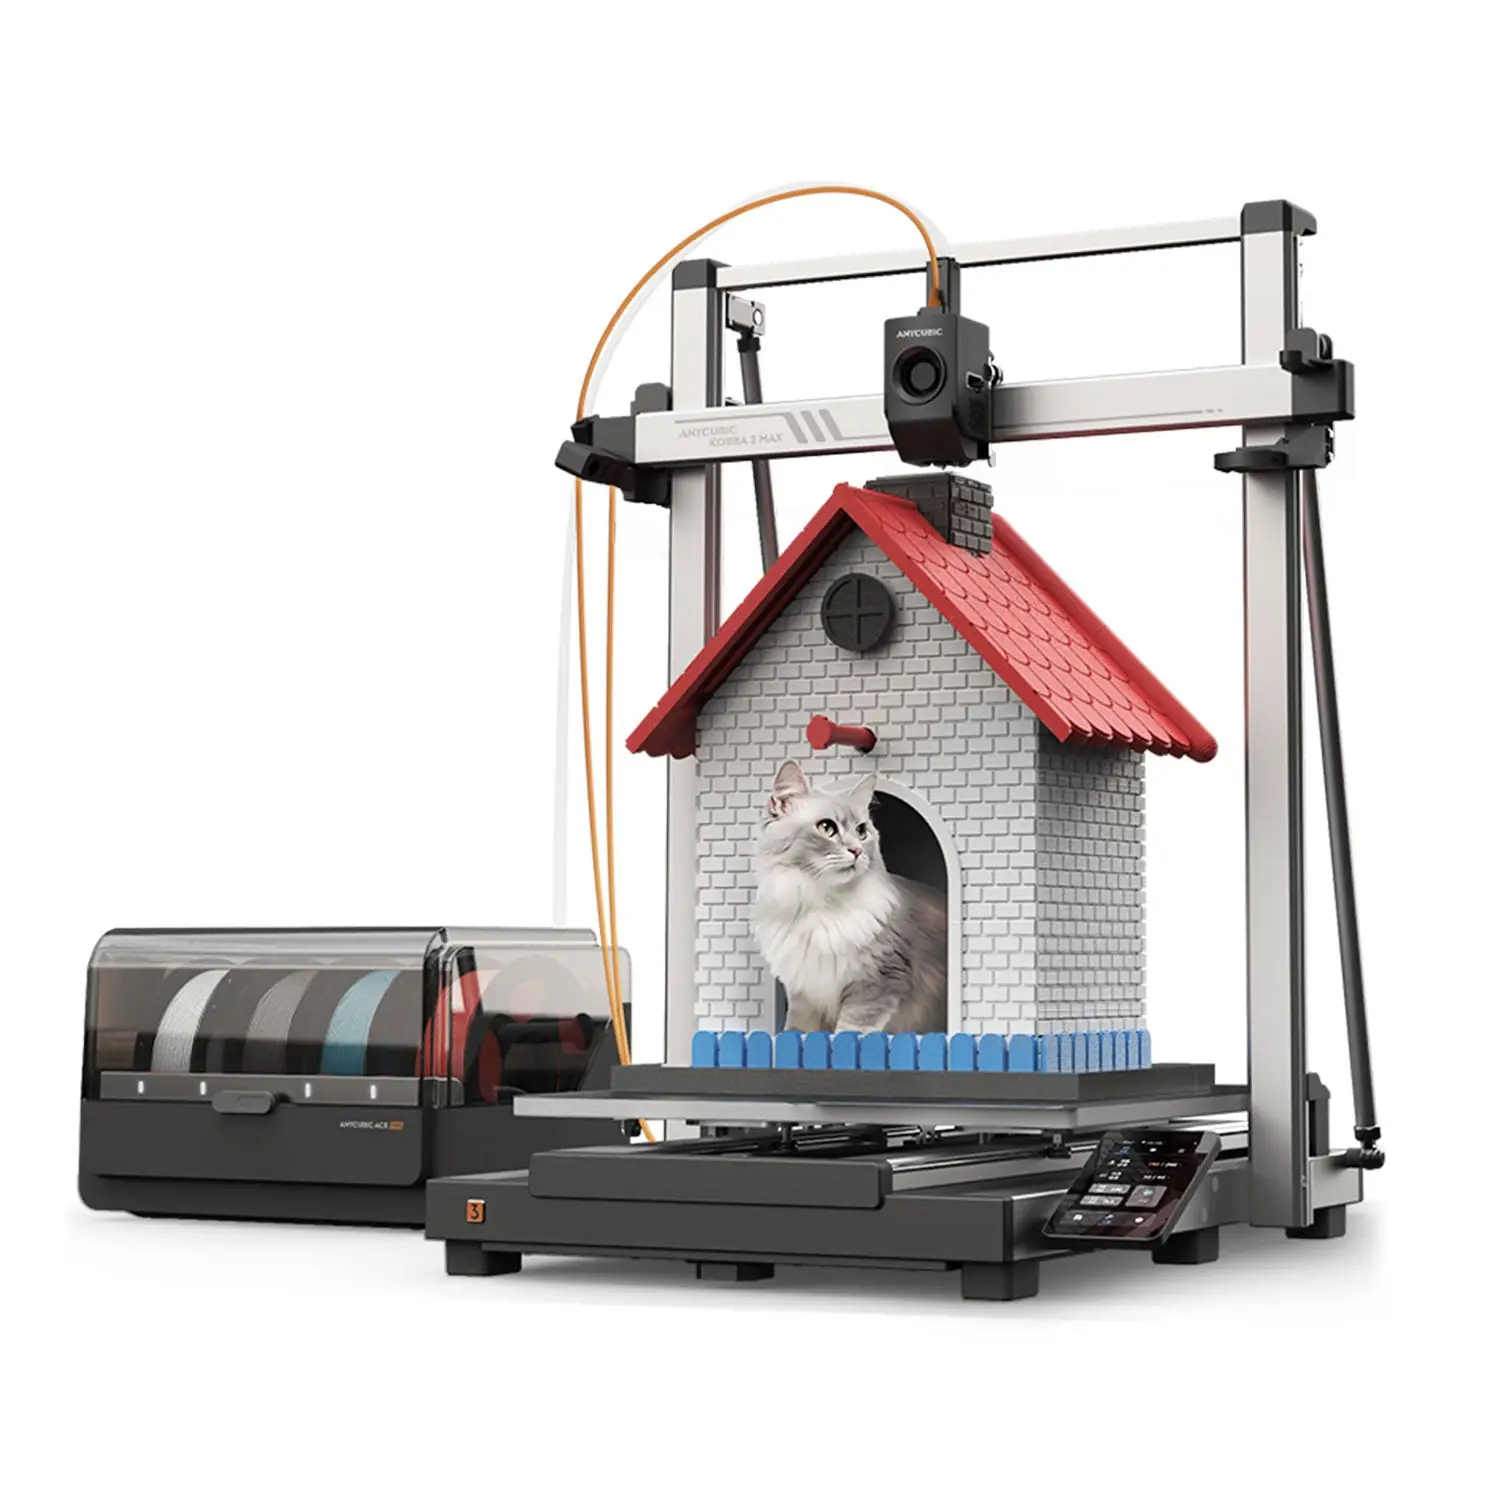
Anycubic Kobra 3 Max Combo offers 420 × 420 × 500 mm, but its moving bed needs substantial front-to-back clearance. Measure spool holders, cabling, bed travel and access to the rear. A large failed prototype consumes far more material than a small fit-check print.
2. Automatic calibration and first-layer consistency
Automatic bed probing compensates for modest surface variation; it does not physically flatten the plate. The Bambu Lab A1 combines automatic calibration with active flow compensation [4], and the FlashForge AD5M advertises one-click leveling [3]. Both features reduce setup work, but consistent adhesion still needs a clean surface.
Auto leveling cannot clean fingerprints, dry wet filament or repair a loose belt. A reliable first layer has continuous lines with slight compression, no gaps and no nozzle scraping. First try the manufacturer’s PLA profile and correct plate setting before changing Z offset or flow.
A removable PEI-coated spring-steel plate makes finished parts easier to release. The FlashForge Adventurer 5M includes one and has quick-detach nozzles [3]. Let the plate cool; using a metal scraper forcefully can damage its coating or cut your hand.
Rule of thumb: Prioritize reliable first layers and accessible replacement parts before paying for a faster motion system.
3. PLA, PETG, TPU and the enclosure question
PLA is the starting material for most users: forgiving adhesion, low warping and many tested presets. Prusa lists approximately 185–235°C nozzle / 50–60°C bed for PLA, versus 215–270°C nozzle / 70–90°C bed for PETG [2]. These are ranges, not instructions to use the maximum; the filament spool and printer profile take priority.
PETG can suit tougher brackets, while TPU is flexible but may need slower loading. Bambu’s A1 specification lists PLA, PETG, TPU and PVA as ideal, but ABS, ASA, PC, PA and fiber-reinforced blends as not recommended, despite its 300°C hotend [4]. Match the whole printer and chamber to the material, not nozzle temperature alone.
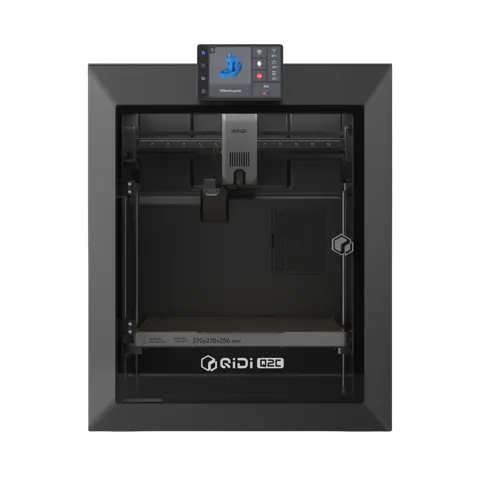
ABS, ASA and many engineering materials are more demanding because drafts cause warping and hot extrusion can emit fumes. Prusa recommends an enclosure for ABS and ASA [2]. The enclosed QIDI Q2C lists 270 × 270 × 256 mm, 370°C nozzle and 120°C bed; still confirm tested material profiles and actual exhaust filtration.
The open ELEGOO Neptune 4 Pro lists a 300°C nozzle, but hotend temperature alone does not provide a warm chamber [5]. FlashForge explicitly says ABS-series filament is not compatible with the standard Adventurer 5M [3]. Check manufacturer-approved materials rather than treating temperature headroom as certification.
4. Advertised speed versus actual print time
Maximum movement speed is not continuous printing speed. Bambu quotes 500 mm/s and 10,000 mm/s² acceleration for A1 [4]. FlashForge advertises 600 mm/s for Adventurer 5M, but its official manual distinguishes 600 mm/s maximum travel from 10–300 mm/s printing speed [3][14]. Compare complete sliced job times, not marketing headline motion.
The slicer also limits acceleration, cooling, cornering and the hotend’s volumetric flow. A 0.45 mm line × 0.20 mm layer × 150 mm/s travel along that line demands about 13.5 mm³/s of extruded plastic. This is a geometry calculation, not a benchmark for any model. Real speed varies with walls, supports and geometry.
The ELEGOO Neptune 4 Pro claims up to 500 mm/s with Klipper control [5]. Compare complete slicer estimates at the same layer height, filament, wall count and surface-quality target. Slowing outer walls can improve surface finish even when infill travels faster.
5. Slicer, repair parts and long-term control
Long-term ownership means access to 0.4 mm nozzles, complete hotends, fans, belts and PEI plates. The Original Prusa MINI+ offers a 180 mm build cube and a repair-oriented ecosystem. Prusa publishes model-specific maintenance instructions, including fan and belt checks [6].
FlashForge lists quick-swap 0.25, 0.4, 0.6 and 0.8 mm nozzles for Adventurer 5M [3]. Smaller diameters favor fine detail; larger ones allow thicker beads on big objects. Layer bonding, cooling and flow still determine whether a part is robust. Check local availability of a complete replacement hotend before relying on a proprietary nozzle.
Check whether slicing and file transfer work by USB, local network or a cloud account. Bambu A1 supports Wi-Fi and microSD storage [4]. Test the exact offline or LAN workflow you need rather than assuming any advertised wireless connection permits independent printing when cloud access is unavailable.
6. Ventilation, noise and where a printer can safely run
FDM printing emits ultrafine particles and volatile compounds, even from common plastics [7]. NIOSH recommends capture near the source, appropriate ventilation and filtration [8][11]. In a 2026 NIOSH study, a fully enclosed filtered setup reached 99.8% minimum particle capture, while a partly enclosed design reached only 28.6% because printer cooling fans bypassed the filter [13]. These are specific laboratory setups, not consumer printer ratings; neither percentage demonstrates removal of all VOCs.
Put a printer on a stable surface in a ventilated area, away from sleeping spaces, children and pets [8][11]. A decorative enclosure does not necessarily control particles or gases: leakage and cooling fans change performance [13]. UL 2904 addresses measured emissions; do not claim certification unless the particular model has it [9].
Hot nozzles and beds burn, and belts can catch fingers or loose cords. Older Bambu A1 units were recalled in the US in June 2024 because damaged heatbed cables could spark, shock or ignite; CPSC identifies affected serial numbers by an “A” in position six [12]. Fan noise and quoted quiet modes never outrank safe placement.
Rule of thumb: Plan ventilation and a stable, unobstructed work area before deciding where the machine will live.
Types compared
| Type | Best when | Main drawback |
|---|---|---|
| Compact open FDM | Small PLA projects and limited space | 180 mm build constraints |
| Standard open bed-slinger | Organizers, brackets, larger household parts | Moving bed needs room |
| Open CoreXY-style | Compact footprint and faster motion | More complex motion mechanism |
| Multi-color open printer | Colored models, signage and decoration | Purge waste and extra loading |
| Large-format printer | Oversize props and prototypes | Space and expensive failed prints |
| Enclosed FDM printer | Material requiring more stable chamber temperatures | Ventilation and complexity still matter |
Budget 3D printers for beginners, small homes, families and heavy use
Beginners: The Bambu Lab A1 mini offers a 180 mm cube, automatic calibration and an included LED Lamp Kit in this specific bundle. The Bambu Lab A1 provides more room without requiring a new learning approach.
Small homes: The FlashForge Adventurer 5M offers a 220 mm cube and a relatively compact motion arrangement. Check spool and service clearance before choosing a shelf.
Families: Make placement and emissions control the main requirements. A removable plate and automated calibration are convenient, but an open printer has exposed hot and moving parts [7][8].
Frequent functional printing: The ELEGOO Neptune 4 Pro provides a 225 × 225 × 265 mm build area and a segmented heated bed. Select materials suited to its open configuration and verify nozzle-part compatibility [5].
Color models: The FlashForge AD5X with IFS includes four-color feeding; use it when colored work is common enough to justify loading time and purge material.
Oversized projects: The Anycubic Kobra 3 Max Combo has a 420 × 420 × 500 mm workspace. Consider split-and-assemble designs before dedicating substantial space to one machine.
Features that are marketing noise
An advertised 600 mm/s does not guarantee shorter high-quality prints. Hundreds of optional profiles, oversized accessory packs and AI failure detection sound helpful but do not replace supervision of the first layer or good slicer settings. Multi-color automation can create more waste than printing and assembling separate pieces.
A hotend rated to 300°C does not guarantee success with ABS, ASA or nylon on an open machine [2][4]. Automatic bed probing is not a substitute for a clean plate. A protective-looking enclosure is not evidence of certified low emissions [9].
Setup tips
- Measure the full printer footprint, including bed travel, spool holder and power cable.
- Position it on a rigid, heat-tolerant surface, away from curtains and sleeping spaces, with ventilation and clearance [7][8][13].
- Remove transport locks and inspect cables before powering on. For used Bambu A1 units, verify that the 2024 heatbed-cable recall was resolved by the approved remedy [12].
- Run the manufacturer’s automatic calibration and original sample print first.
- Load ordinary 1.75 mm PLA with a matching slicer profile and nozzle size [2].
- Watch the entire first layer; adjust adhesion problems before committing to a long print.
- Allow the plate to cool before removing parts, then clean it using the manufacturer’s approved method.
- Back up a successful profile and compare sliced time, supports and material use before large jobs.
Maintenance and what wears out
After prints: Remove loose filament and scraps; keep the build plate clean. Prusa recommends checking the hotend, motion components and fans regularly, with model-specific instructions [6]. A cleaner safe for glass may damage some textured or coated surfaces.
Filament storage: Seal dry spools with desiccant; passive storage does not actively remove absorbed moisture. Prusa suggests 45°C for six hours for PLA and 55°C for six hours for PETG for its materials [10]. Follow the actual filament maker’s guidance and check spool heat tolerance: some cardboard-core spools can loosen when heated.
Wear items: Nozzles, gears, belts, fans, bearings and PEI sheets deteriorate. Filled filaments wear nozzles faster; some fiber-filled spools require hardened nozzles [2]. Prusa recommends checking fans and drive components after a few hundred printing hours on certain models [6]. Use the schedule for your exact printer, not a universal interval.
Annual running costs: 2 kg per year means two ordinary 1 kg filament spools, while 1 kg per month means 12 kg/year, excluding failures and color-change purge. A hypothetical average draw of 120 W for 300 hours uses 36 kWh/year; this is not a measured model result. Budget for nozzles, plates, desiccant and ventilation filters, whose replacement intervals depend on use.
Service life: Machines can last years, but abrasion, bearings, heat and parts supply prevent a universal lifespan prediction. For secondhand printers, inspect the power cable and hotbed wiring, verify recalls, and confirm that correct nozzles, fans and belts remain obtainable [6][12].
Rule of thumb: Diagnose plate cleanliness, wet filament and nozzle wear before changing an entire printer or buying upgrades.
Common mistakes
Buying excessive build volume; mistaking travel speed for extrusion speed; adding four-color printing before one-color reliability; assuming leveling cleans a plate; printing ABS on an unsuitable open machine; assuming PLA is emission-free; buying a recalled used A1 without confirming its remedy; or overlooking nozzles, plates and purge waste [2][7][8][12][14].
- Bambu Lab A1 mini — compact 180 mm starter printer with automatic calibration.
- Bambu Lab A1 — versatile 256 mm work area for practical household parts.
- FlashForge Adventurer 5M — 220 mm CoreXY-style printer with quick-change nozzles.
- ELEGOO Neptune 4 Pro — 225 × 225 × 265 mm work area with mesh leveling.
- FlashForge AD5X with IFS — built-in four-color hardware for decorative prints.
- Anycubic Kobra 3 Max Combo — large-format 420 × 420 × 500 mm printing.
Sources
[1] Bambu Lab — A1 mini Specifications [2] Prusa — Filament Material Guide [3] FlashForge — Adventurer 5M Specifications [4] Bambu Lab — A1 Technical Specifications [5] ELEGOO — Neptune 4 Pro Specifications [6] Prusa — Regular Printer Maintenance [7] EPA — 3D Printing Research and Emissions [8] CDC NIOSH — Characterizing 3D Printing Emissions and Controls [9] UL — UL 2904 3D Printer Emission Standard [10] Prusa — Drying Filament [11] CDC/NIOSH — 3D Printing with Filaments: Questions on Emissions and Controls [12] US CPSC — 2024 Bambu Lab A1 Heatbed-Cable Recall [13] CDC NIOSH — 2026 Study of Four 3D Printer Emission Controls [14] FlashForge — Adventurer 5M Manufacturer Manual (PDF)
See also: Budget 3D Printers under $300 (2026) · Budget 3D Printers under $500 (2026)