How to Choose a Multi-Toolhead 3D Printer in 2026
Published October 31, 2026
Products in this guide
In this article
Choose a multi-toolhead 3D printer for repeat material changes, clean support interfaces or different nozzles on one model. Fast swaps do not guarantee fast finished prints, while four loaded spools do not necessarily mean four independent nozzles [15][20]. Compare toolchangers with shared-nozzle feeders, then check alignment, size, ventilation and repair parts.
Is a multi-toolhead 3D printer worth it in 2026?
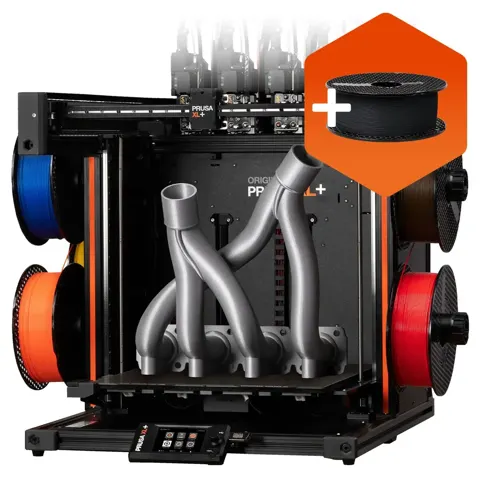
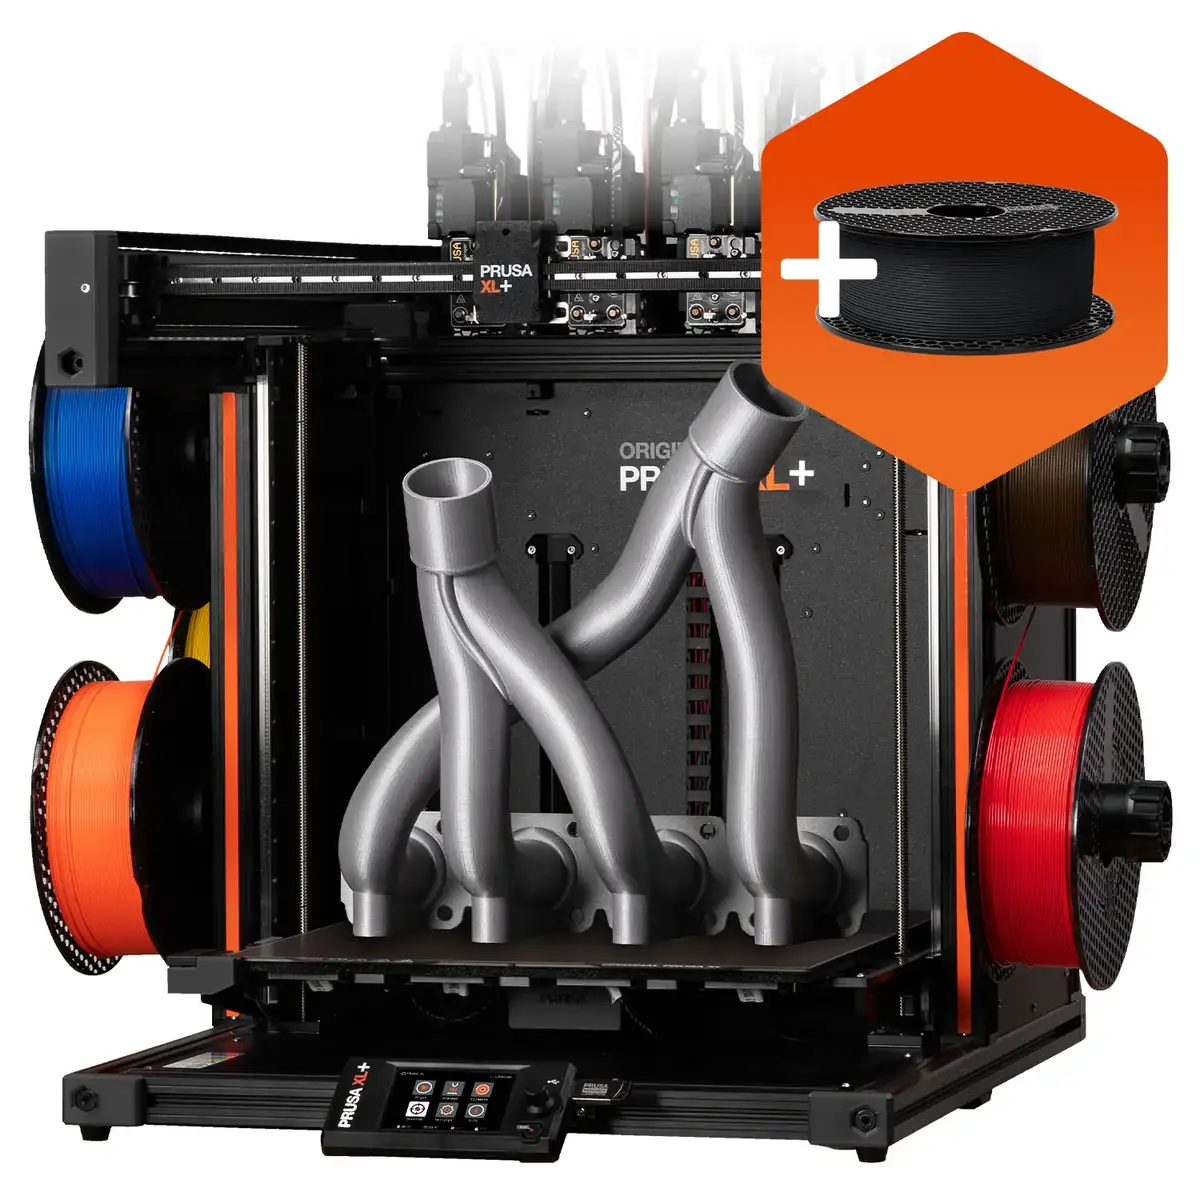
Worth it for frequent multi-material or mixed-nozzle jobs. Dedicated hotends reduce color cross-contamination and can keep support or flexible filament separate. Even two distinct material roles may justify a toolchanger; you do not need to fill four or five heads. The Prusa XL Five-Toolhead has 360 × 360 × 360 mm volume. Prusa’s August 13, 2026 XL+ refresh introduced a faster offset sensor, GT1.5 belts, improved cooling, high-flow nozzles and a nozzle wiper [16]. Check whether a listing is for an older XL or an XL+; both have received firmware 8.0.0 dated October 22, 2026 [21].
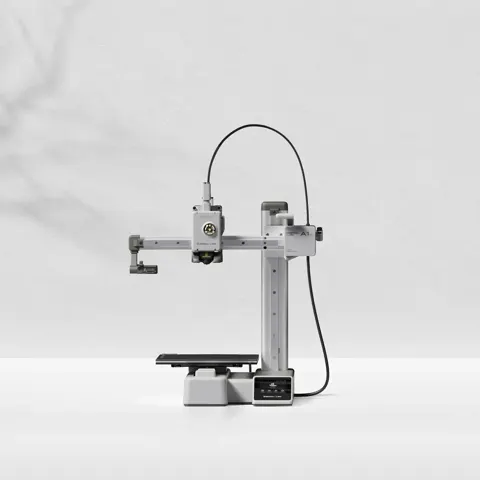
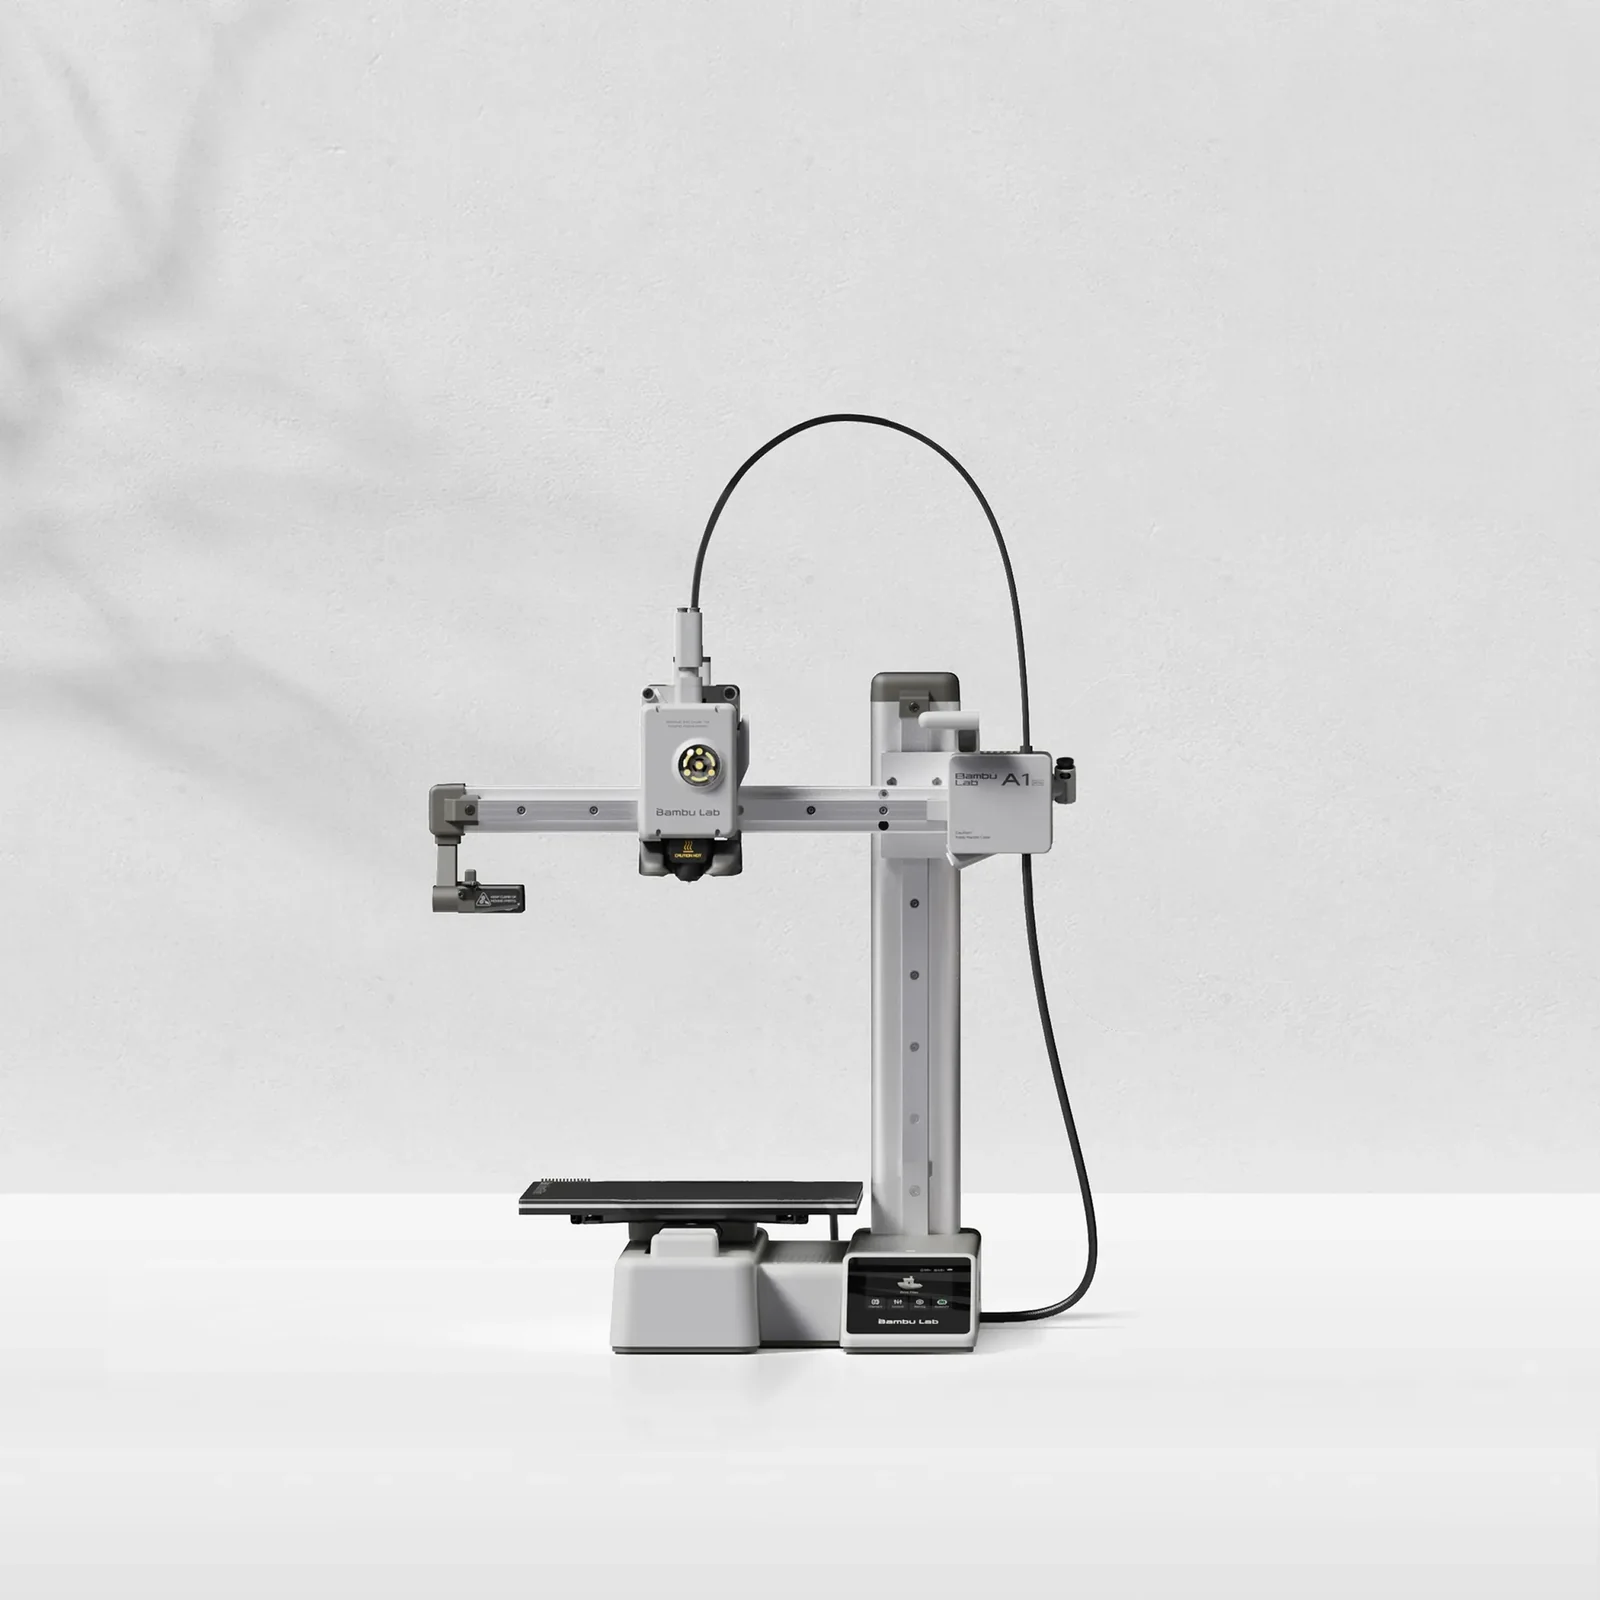
Skip toolchanging for occasional color accents or mostly single-color PLA. The Bambu Lab A1 mini Combo feeds four spools into one nozzle, with 180 × 180 × 180 mm build volume. Its simpler architecture avoids toolhead docks but adds filament flushing at color transitions.
What actually matters
1. The number of independent hotends
A four-head machine parks four separately equipped nozzles. A five-head machine makes room for another material or nozzle diameter: four colors plus a dedicated support interface is a concrete five-tool use case. Count distinct roles in the projects you actually slice, not how many spools look appealing.
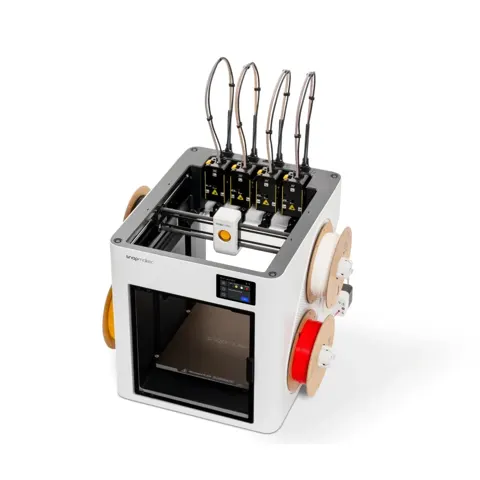
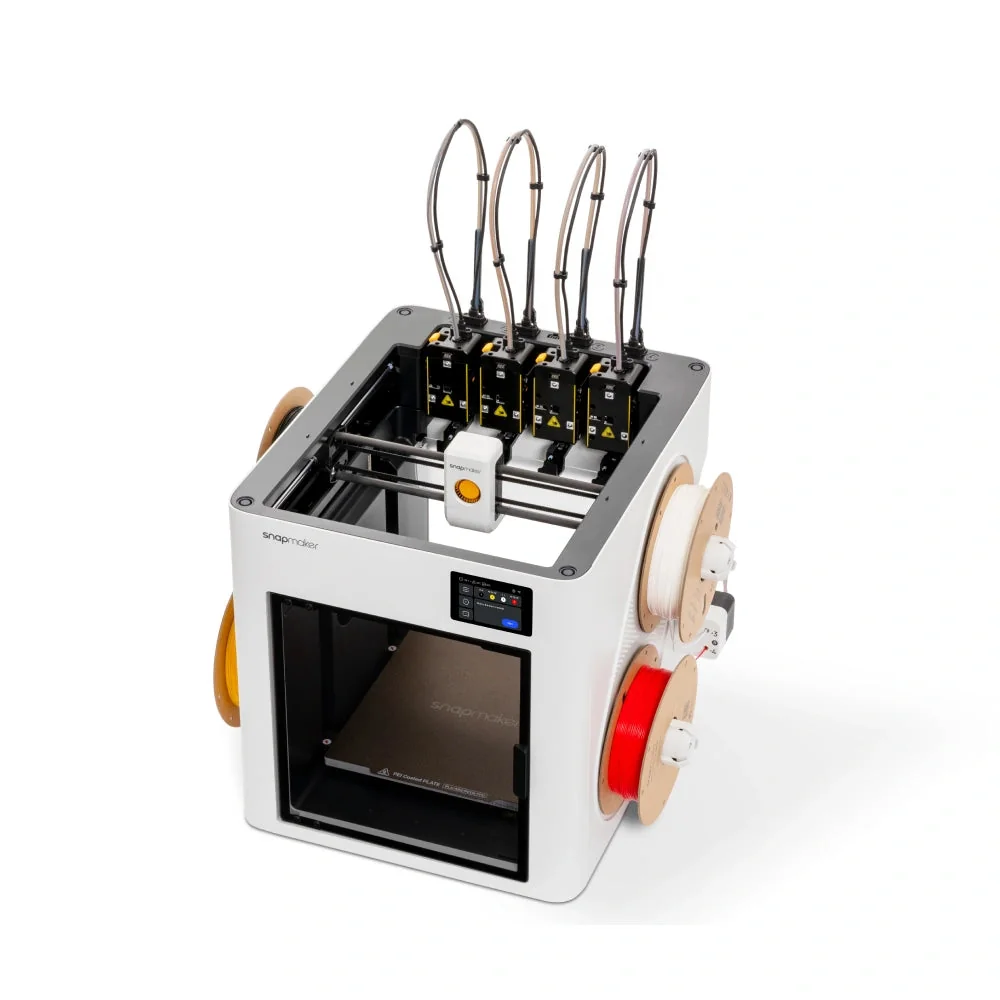
A toolchanger parks a whole hotend; a shared-nozzle feeder unloads filament and flushes the melt path. Prusa enables the XL wipe tower by default for reliable changes [1]. Snapmaker advertises five-second swaps and up to 85% less waste in selected tests [15]. Its ‘zero purge’ U1 still prints a small prime tower to clear degraded filament from parked nozzles [20]. Compare identical sliced jobs, including supports and towers.
Rule of thumb: Even two different hotend roles can justify a toolchanger; for occasional color changes, compare sliced total print time and waste before buying extra heads.
2. Build volume and physical footprint
Compare your largest one-piece design with actual X, Y and Z travel. A 270 mm axis cannot fit an uncut 300 mm-wide part. Account for tubing, dry boxes, parked tools, moving beds and doors rather than measuring only the heated plate.
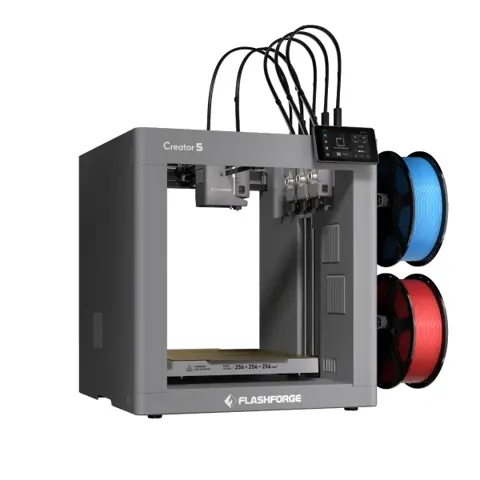
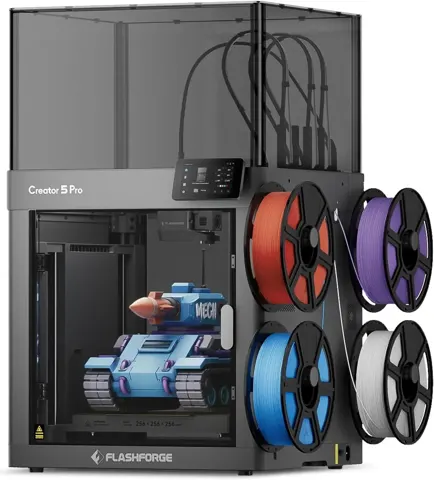
The Snapmaker U1 provides 270 × 270 × 270 mm in about 584 × 499 × 730 mm of installation envelope [15]. The open FlashForge Creator 5 and heated Creator 5 Pro both offer 256 × 256 × 256 mm. FlashForge lists the Pro at 520 × 443 × 710 mm, including filament tubes and holders [22]. The Prusa XL reaches 360 mm along each axis [14].
3. Material temperature, enclosure, and nozzle
A 0.4 mm nozzle is a broadly useful starting point; PrusaSlicer suggests a maximum practical layer height near 0.32 mm for that nozzle [3]. A 0.6 mm nozzle can lay wider extrusion for larger functional parts but sacrifices some tiny detail. For abrasive carbon- or glass-filled material, use a hardened nozzle and verify other filament-path components are suitable [4].
PLA: commonly around 185–235°C nozzle / 50–60°C bed. PETG: roughly 215–270°C nozzle / 70–90°C bed; check each actual spool rather than treating these as required profiles. ABS, ASA, PC and some nylons need more stable enclosure temperatures to limit warping [5][6]. A nozzle marked 300°C does not by itself establish that a printer handles engineering polymers well.
The FlashForge Creator 5 Pro offers 65°C active chamber heating, 320°C nozzle, 120°C bed and H13 HEPA plus carbon filters [22]. Its open-frame Creator 5 does not offer the same temperature control. FlashForge’s Pro has a cooling mode for PLA/PETG and a heating mode for warping-prone polymers [22]. Filters are not a substitute for local extraction and ventilation [11][12]. Crucially, the Prusa XL+’s 60°C enclosure heater was announced as upcoming, not necessarily included or available, in the August 2026 update [16].
4. Toolhead calibration and repeatable docking
Every head needs repeatable X/Y registration and Z offset; errors cause doubled color edges, weak joins or nozzle scraping. Prusa reports its XL+ eddy-current sensor replaces the mechanical offset pin and calibrates about 20 times faster [16]. That is a calibration-time claim, not twentyfold better print accuracy. Recheck after nozzle replacement, crashes or belt work. XL+ support lists firmware 8.0.0 dated October 22, 2026 [21].
5. Filament handling and slicer compatibility
PVA, PETG and nylon can absorb moisture, producing stringing, weak extrusion or ooze from idle nozzles. Use sealed storage and a correctly set filament dryer where required. Desiccant helps storage but does not always restore a wet spool [7][19]. A toolchanger’s purge advantage decreases when damp filament leaks while parked [1].
The slicer must handle materials, idle temperatures, support interfaces, wipe structures and offsets. Prusa documents successful PLA/PETG breakaway support combinations, but their weak mutual bonding makes them unsuitable as automatically reliable structural layers. Test interfaces, temperatures and adhesion with the actual materials [8].
6. Repairs and total time to a usable part
Confirm spare hotends, heaters, sensors, fans, belts and dock parts are actually orderable for the exact printer. Four heads multiply wear and calibration points. Compare complete sliced time and waste, including warm-up, tool changes, towers, supports and post-processing, not maximum travel speed.
Types compared
| Type | Best when | Main drawback |
|---|---|---|
| Single-nozzle, single-color FDM | Basic prototypes, fixtures, learning CAD | Manual changes for multi-material work |
| Single nozzle with multi-spool feeder | Occasional decorative multicolor prints | Purge waste and longer change sequences |
| Fixed dual-extruder or IDEX | Two materials or duplicated small parts, where supported | Two-nozzle limits and possible ooze or calibration work |
| Four-head toolchanger | Frequent multi-color work and several filament properties | More heads, docking, storage, and service points |
| Five-head toolchanger | Four colors plus support, or five distinct roles | Larger investment and added upkeep |
| Enclosed, heated-chamber toolchanger | Advanced polymers and repeatable controlled conditions | Ventilation, operating space, and more complexity |
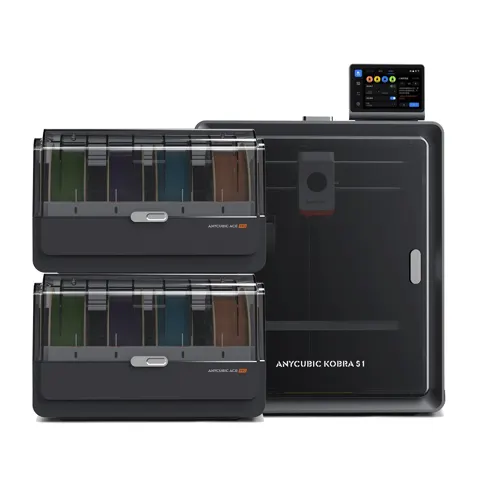
A multicolor feeder such as the Anycubic Kobra S1 Combo (4-Color) is not a substitute for independent hotends when nozzle temperatures or material contamination are the problem. Conversely, a toolchanger does not automatically solve poor adhesion between incompatible plastics.
Multi-toolhead 3D printers for beginners, small homes, families, and heavy use
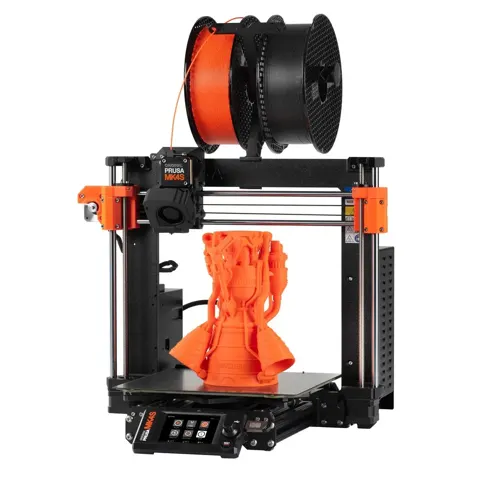
For beginners: Learn bed adhesion, slicing and first layers first. The Original Prusa MK4S DIY Kit avoids toolchanger complexity but requires assembly. For occasional four-color figurines, a feeder system may be simpler than four hotends.
For small homes: Measure spool racks, door swing, feed tubes and service clearance. Use a ventilated space outside bedrooms. NIOSH recommends local exhaust or ventilated enclosures to control printing emissions [11][23]. HEPA filters target particles, while activated carbon targets some gases; a filter installed inside the printer does not guarantee safe indoor air.
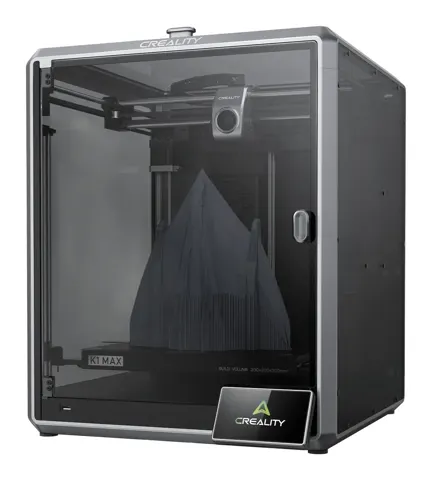
For families and schools: Prefer accessible guards, predictable pause/restart behavior, and an easy-to-clean build surface. Treat hot nozzles, electrical components, moving axes, and emitted particles as real hazards. Supervision and a safer room setup matter more than a colorful phone app. For heavy use or small production: Count failed parts, operator minutes, and turnaround time per batch. The FlashForge Creator 5 Pro (4-toolhead) is a different proposition from its open-frame counterpart if chamber control is a recurring requirement. A large single-head Creality K1 Max, with a 300 x 300 x 300 mm workspace, may be the more practical tool for larger single-material pieces. If a toolchanger sits idle between occasional color jobs, its extra complexity is not earning its keep.
Features that are marketing noise
Maximum motion speed: A headline 500–700 mm/s may mean travel, not continuous extrusion. Creator 5 Pro lists 600 mm/s travel, 300 mm/s printing and 32 mm³/s maximum flow [22]. Geometry, cooling, acceleration and head swaps reduce real throughput. Compare identical sliced jobs, including prime towers and support cleanup.
Zero-waste language: Independent nozzles reduce color-change flushing, not prime towers, supports, failures or first-layer cleaning. Snapmaker explains why its ‘zero purge’ U1 still prints a prime tower [20]. Prusa keeps XL’s wipe tower enabled by default [1]. Evaluate each proposed model in the slicer.
A nozzle’s maximum temperature as a material guarantee. A hot nozzle does not make an open, drafty printer equivalent to a temperature-controlled enclosure. Check bed temperature, chamber design, drying, nozzle wear, and the manufacturer’s validated profiles. [5][6]
Setup tips
- Pick a stable location. Use a rigid surface with room behind and beside the printer. Check mains power, manufacturer clearance requirements, and the path for ventilation or filtered exhaust. Avoid placing the printer next to an air return that spreads emissions.
- Check each tool individually. Load dry filament, confirm tool identification, complete first-layer calibration, and print the same small test on every head before combining them.
- Test docking and offsets. Print a simple two-material registration pattern, then a four-head test if you need four roles. Inspect edge alignment and the underside of support interfaces before committing to a long job.
- Use known profiles first. Start with the slicer vendor’s conservative 0.4 mm nozzle settings and a roughly 0.20 mm layer height where supported. Change one variable at a time instead of copying aggressive demonstration settings. [3]
- Verify support removal. Print a modest bridge or overhang with the chosen support material. If using PLA/PETG breakaway interfaces, confirm the contact surfaces release cleanly rather than assuming every mixture works. [8]
Rule of thumb: Run one small multi-material calibration and one representative overnight-length job before relying on any new toolchanger for scheduled production.
Maintenance and what wears out
After each print: Clear loose scraps, inspect the build plate, look for nozzle ooze and stringing near parked tools, and check that filament routes move freely. Follow the correct plate-cleaning instructions for your specific surface; not every sheet tolerates the same solvent.
Every few hundred hours: Inspect belts, rails, fans, feed gears, wiring, dock faces and build surfaces. For the original XL, Prusa recommends inspections at 200–300 printing hours, linear rail lubrication every 3–6 months, and Z leadscrew lubrication around 500 hours [13]. Never apply generic grease to linear rails; use the specified kit. These intervals are not universal for other printers.
Consumables: Normal filament use dominates the recurring material budget for ordinary projects. Nozzles, build sheets, cleaning supplies, desiccant, and filtration media add costs at intervals dependent on workload and material. Carbon- and glass-filled filament can accelerate wear on a non-hardened nozzle; spare heads make this especially important to plan. [4]
Yearly running use: 50 g filament per week totals 2.6 kg/year before towers, supports and failures. Snapmaker reports 117.8 W average for single-color PLA versus 127.4 W for four-color PLA in its U1 tests [20]; these are manufacturer tests, not universal averages. At 100 W for four hours per week, consumption is 20.8 kWh/year. Heated chambers, dryers and extraction add more. Measure at the wall and budget for nozzles, sheets, desiccant and filters.
Expected life: There is no reliable universal lifespan. Serviceable machines may last years, but fans, belts, nozzles and docks wear sooner. Check parts and manuals; downtime can overwhelm filament savings.
Dry filament: Keep spools sealed with desiccant; a storage box need not remove absorbed moisture. Prusa recommends 45°C for six hours for its PLA and 55°C for six hours for its PETG, subject to spool construction [7]. Follow your filament manufacturer’s limits.
Common mistakes
Buying on head count alone. One-color PLA does not benefit from idle tool docks. Compare completed parts, setup time and spare-parts access before choosing extra nozzles.
Ignoring slicer and filament compatibility. A supported temperature range does not establish that two polymers will bond or that soluble supports will print reliably with the chosen profiles. [8]
Forgetting drying and storage. Wet filament can cause drool from idle nozzles and ruin a carefully calibrated tower-free job. [1][7]
Choosing an open printer for warping-prone ABS or ASA. Stable chamber heat may matter more than another tool [6]. The XL+ enclosure can reach around 50°C passively, while the 60°C active heater was announced as upcoming, not included as standard [16].
- Original Prusa XL (5-toolhead) — for frequent five-role jobs and users who need its 360 mm cubic build area.
- Snapmaker U1 (4-toolhead) — for users prioritizing four independent tools in a 270 mm cubic workspace.
- FlashForge Creator 5 (4-toolhead) — for open-frame four-tool workflows where an actively heated chamber is not required.
- FlashForge Creator 5 Pro (4-toolhead) — for buyers who specifically need a listed heated and filtered enclosure.
- Bambu Lab A1 mini Combo — for small multicolor hobby prints through a four-spool feeder rather than independent toolheads.
- Anycubic Kobra S1 Combo (4-Color) — for buyers comparing enclosed feeder-based multicolor against true tool swapping.
Sources
[1] Prusa: Printing without a purge tower on the XL
[2] Snapmaker: Toolchanger guide and U1 workflow
[3] Prusa: Layers and perimeters, nozzle-to-layer height
[4] Prusa: Composite materials and hardened nozzles
[5] Prusa: Filament material guide and printing temperatures
[6] Prusa: When an enclosure is needed
[7] Prusa: Drying filament and preventing moisture
[8] Prusa: Combining materials on the XL
[9] Formlabs: FDM vs. SLA, labor and ownership considerations
[10] Prusa: Original XL+ firmware and hardware support
[11] CDC/NIOSH: Safe 3D printing for schools and makerspaces
[12] UL Research Institutes: 3D-printing emissions and controls
[13] Prusa: Regular XL printer maintenance
[14] Prusa: XL+ five-tool specifications and availability
[15] Snapmaker: U1 four-tool system, five-second changes and comparative waste caveats
[16] Prusa: August 13, 2026 XL+ update and new alignment sensor
[17] FlashForge: Creator 5 Pro enclosure, chamber heating and filtration specifications
[18] Chemical Insights: 3D-printing emissions and engineering controls
[19] FlashForge: Creator 5 Filament Use and Chamber Temperature
[20] Snapmaker U1 FAQ: Why Zero Purge Still Uses a Prime Tower
[21] Prusa XL+ Support: Firmware 8.0.0, October 22, 2026
[22] FlashForge Creator 5 Pro Official Specs: Size, Speed, Heating, Filters
[23] NIOSH: Safer 3D Printing Controls for Workplaces
See also: 3D Printers under $300 (2026) · 3D Printers under $500 (2026)